Paper Mill Equipment Tailing Pulp Pressure Screen Solutions

The tailing pulp pressure screen works in tough conditions compared to the main screening stage. The pulp has higher impurities, shorter fibers, and more stickies. The most common problem for a tailing pulp pressure screen is balancing fiber recovery and impurity discharge. Reject thickening is a major issue. If the discharge is not handled well, high-concentration rejects will build up and cause screen blinding. A low reject rate causes heavy clogging and can damage the screen basket and rotor. A high reject rate causes good fiber loss. Also, sticky impurities can pass through the slots, causing paper defects.
To fix these problems with your tailing pulp pressure screen, you need practical solutions. First, adjust the reject rate based on the actual pulp conditions. Do not use a fixed value. Second, add dilution water at the reject end. This lowers the concentration and helps impurities flow out smoothly. Third, design the reject pipe well. Put a drain pipe at the lowest point and adjust the valve to stop bottom clogging. The table below shows a simple guide to these problems and solutions for the tailing pulp pressure screen:
| Problem | Cause | Solution |
|---|---|---|
| Screen Blinding | Low reject rate causes high concentration | Adjust reject rate dynamically |
| Reject Thickening | Water passes through the screen | Add dilution water at the reject end |
| Fiber Loss | High reject rate | Find the right balance for the pulp |
| Pipe Clogging | Poor pipe design | Add a drain pipe at the lowest point |
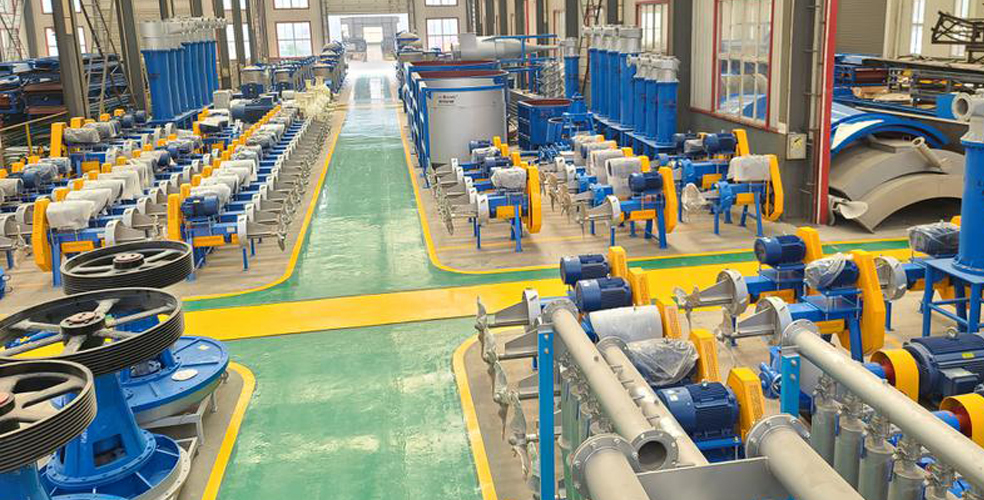
We offer this high-quality tailing pulp pressure screen and other paper mill equipment. Our tailing pulp pressure screen is built for stable operation and easy maintenance. We supply complete paper production lines for different paper grades. We also provide turnkey paper production line services. If you need a reliable tailing pulp pressure screen for your paper making machine, we can help. Contact us for more information.
Email: leizhanworld@gmail.com